A hair brush sample can look right in a photograph and still create expensive problems after the first production run. Bristles can work loose, a cushion can feel too soft or too firm, a wooden handle can develop a rough edge after a change in humidity, and a carton can allow the finished brush to arrive scratched.
For a private-label buyer, the purpose of quality control is not to make every brush identical down to a microscopic level. It is to agree which characteristics are critical to the customer experience, make them measurable, and approve those points before the factory starts mass production.
Buyer’s note: Approve the physical sample, material specification and packaging together. This checklist is a production framework; confirm the final requirements for your target market before mass production.
This checklist is designed for paddle brushes, cushion brushes, pin brushes and boar-bristle blends. It is a practical approval framework, not a substitute for the buyer's own safety, chemical or market-specific compliance requirements.
Start with a written “golden sample”
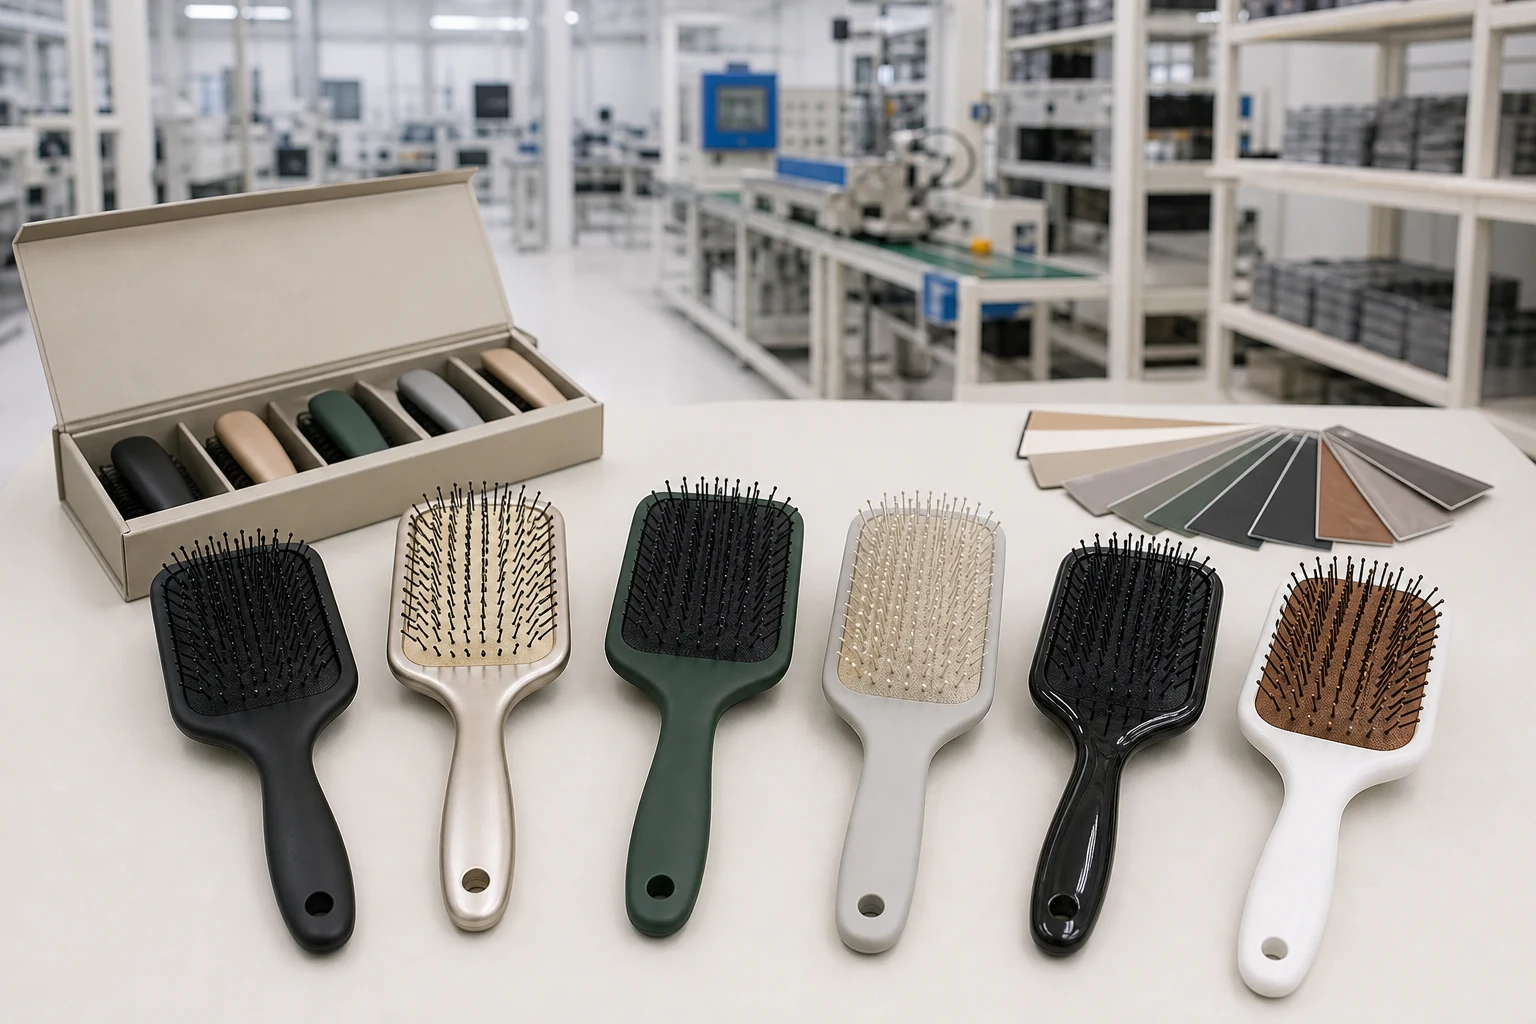
Before discussing inspections, create one approved reference sample. It should identify the exact combination of handle material, brush head, bristle specification, colour, logo position, coating, packaging and accessories.
The golden sample prevents a common sourcing problem: a buyer approves a general style, while the production team interprets the details differently. Attach photographs from several angles and record the following in the purchase specification:
- Brush type and overall dimensions, including acceptable tolerances where they matter.
- Handle material and finish: for example beech wood with clear coating, bamboo with a matte oil finish, or moulded ABS with a soft-touch finish.
- Bristle construction: nylon, boar bristle, mixed bristle, metal pin, ball tip, loop or other format.
- Bristle layout, hole count or tuft pattern, plus the expected feel on the scalp.
- Logo artwork, colour reference and printing/engraving position.
- Inner packaging, master-carton arrangement and barcode or label location.
If the project involves a new mould, the approved sample should also state what is provisional. A 3D-printed handle, for example, is useful for shape and logo placement but does not prove injection-moulded surface finish or production-cycle stability.
The 10-point quality-control checklist
| Check | What the buyer should inspect | Why it matters |
|---|---|---|
| 1. Dimensions and silhouette | Compare length, head width, thickness and visible shape with the approved sample. | A small shape change can alter grip, packaging fit and perceived value. |
| 2. Bristle or pin retention | Pull-test representative tufts or pins using an agreed method; inspect for movement after normal brushing strokes. | Loose bristles create complaints and can make a brush unsafe to use. |
| 3. Cushion rebound | Press several positions across a cushion brush and confirm a consistent return without permanent dents or rubbing. | Uneven rebound changes scalp feel and can expose the cushion edge. |
| 4. Tip and scalp contact | Check ball tips, rounded nylon ends or natural-bristle finishing for burrs, sharp points and missing tips. | This is the point of direct contact with the user. |
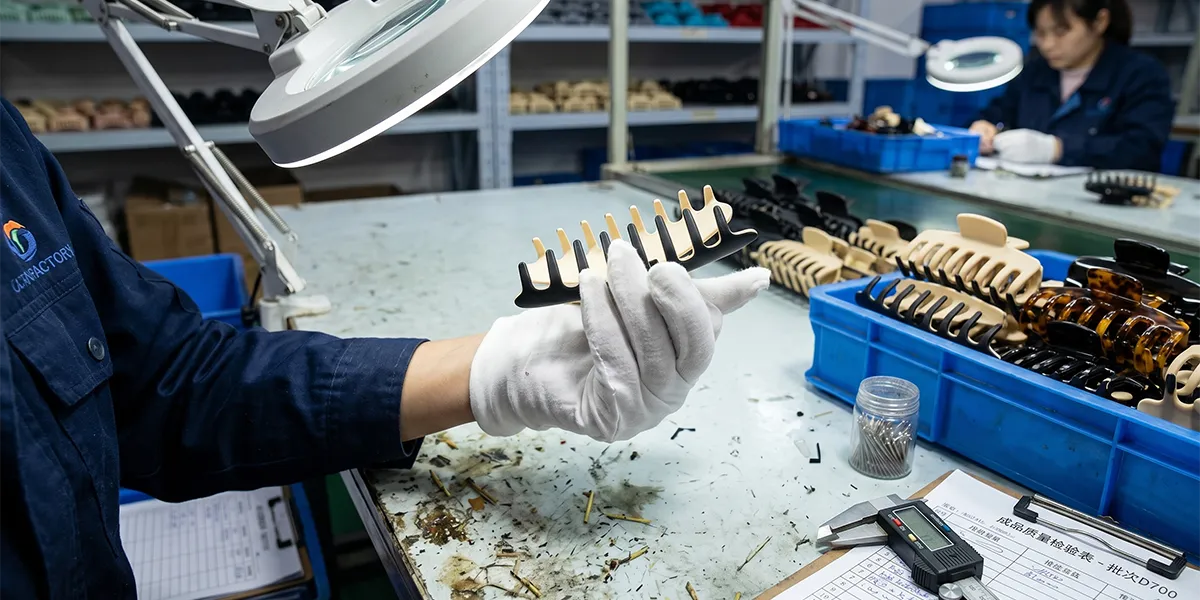
| 5. Handle finish | Inspect under strong light and by touch for rough grain, coating runs, sink marks, flash, scratches and colour variation. | The handle is the most visible private-label surface. |
| 6. Joint security | Twist or apply normal handling force at the head-to-handle joint and inspect glue lines, fasteners or clips. | A weak joint may fail after transport or repeated use. |
| 7. Odour and material cleanliness | Open a newly packed brush and check for unusual odour, dust, oil, excess glue or loose fibres. | It is an early warning for material, curing or packing issues. |
| 8. Logo and decoration | Compare artwork, contrast, position and rub resistance with the approved artwork file. | A good brush with a poor logo still fails as a private-label product. |
| 9. Packaging protection | Check whether the individual pack prevents bristle deformation and whether master cartons prevent movement. | Many cosmetic defects occur after final inspection, during shipping. |
| 10. Lot records and sampling | Ask the factory to record production date, lot, inspection quantity, defect types and corrective action. | Records make an issue traceable instead of anecdotal. |
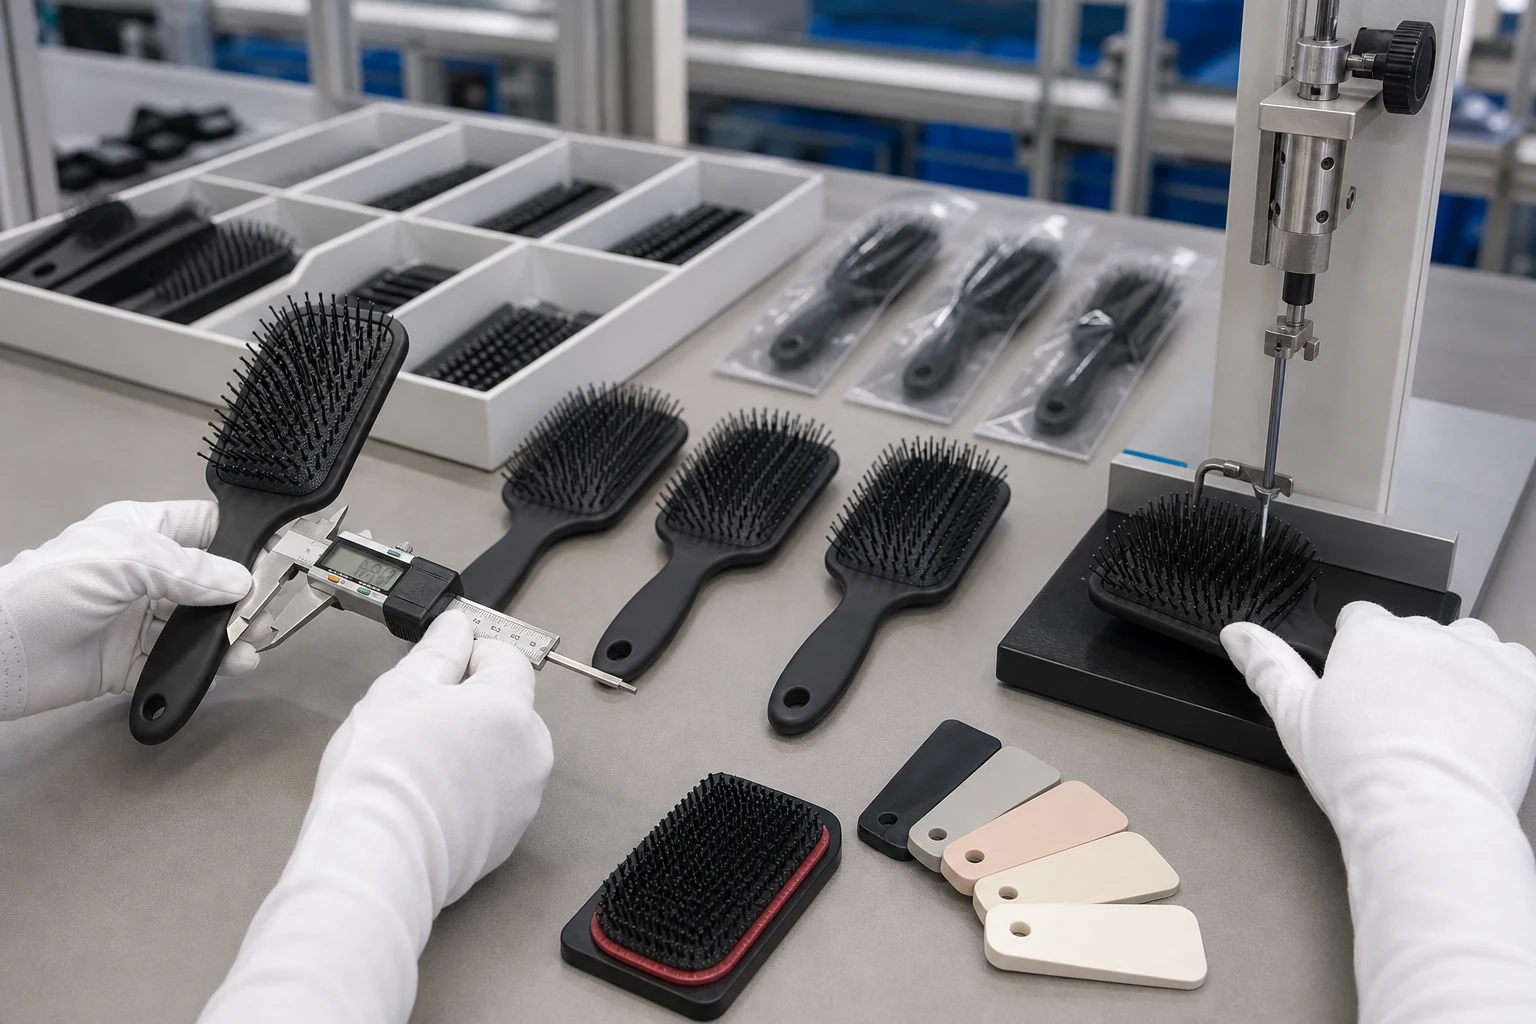
1. Inspect bristle retention before judging appearance
For a pin or nylon brush, retention is one of the first checks to agree. The buyer and factory should decide the test method before production—not after a complaint. The method might specify the test point, pull direction, number of samples and whether a single loose pin is a critical, major or minor defect.
For a mixed boar-bristle brush, inspection also needs to distinguish normal loose trimming fibres from an actual tuft that is pulling out of the base. The factory should clean the brush after trimming so the buyer is not judging production dust as product shedding.
If you are still deciding which bristle system fits the product, compare the trade-offs first in the custom brush bristles guide. The bristle material, anchor method and brush base must be specified together; choosing them separately often produces an unstable design.
2. Test cushion rebound in more than one place
A cushion brush should not be tested only in the centre. Press near the top, bottom and both sides, then inspect the perimeter where the cushion meets the brush body. Look for air leakage, an uneven surface, a loose edge or a cushion that stays depressed.
The goal is not necessarily a hard or a soft cushion. Different products deliberately use different resistance. The key is that the approved sample defines the intended feel and that production brushes remain consistent with it.
For a new brush head, ask the factory to send a small pre-production sample set rather than a single piece. Several samples reveal whether the process is repeatable.
3. Treat handle finish as a functional check
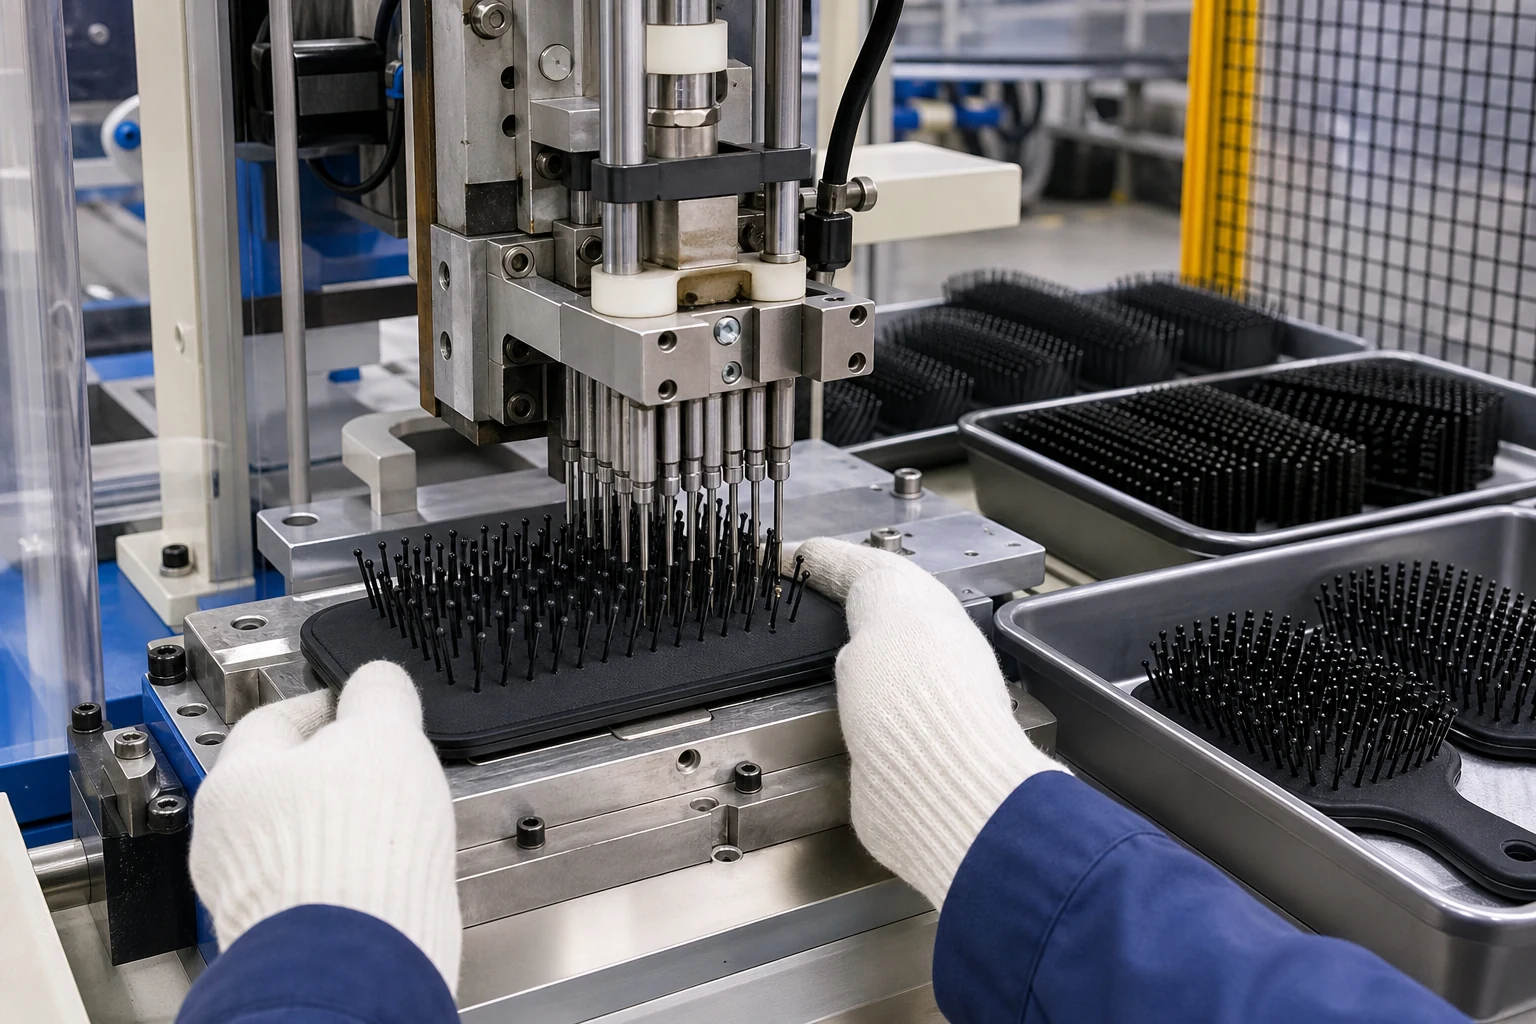
Wooden, bamboo and cork-handled brushes need an extra review after the finish has fully cured. Check for splinters, rough end grain, uneven stain, coating that feels tacky and colour variation beyond the approved range. For moulded plastic handles, inspect parting lines, flash, sink marks and the seam around any insert.
It is helpful to photograph defects under a consistent light source and label them in the approval file. “Finish is not good” is difficult to act on; “visible flash at the underside seam” is clear to the production team.
4. Confirm decoration early, especially on curved surfaces
Logo printing, hot stamping, laser engraving and pad printing behave differently on wood, plastic and curved surfaces. Do not approve a flat artwork proof as the final logo approval. Approve the mark on the actual handle material and curve.
The same rule applies to colour. A digital image is not a production colour standard. Where colour matters, approve a physical reference or a defined colour system and state which surface finish it applies to: glossy, matte, coated wood or textured plastic.
5. Include packaging in the production approval
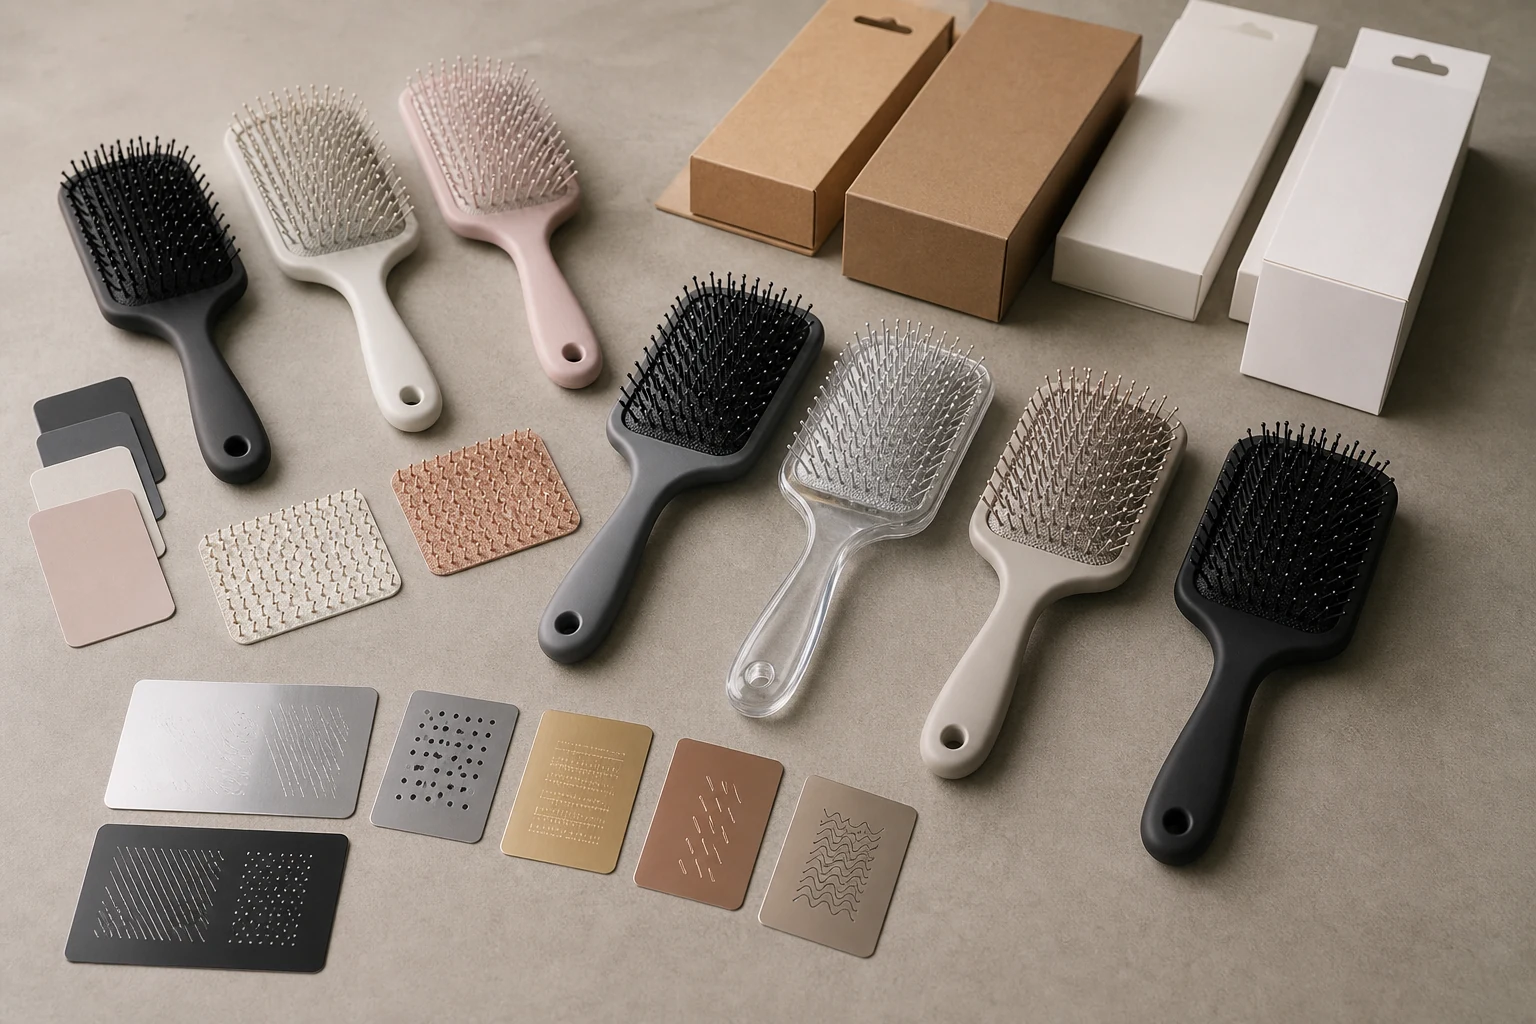
Packaging is part of the product specification. A brush with protected bristles may need a tray, sleeve, window box, bag or head cover depending on the material and sales channel. The master carton should prevent the individual packs from sliding, crushing or rubbing against each other.
Ask for photographs of a packed carton and, for large orders, a small packed sample shipment before finalising the carton artwork. This is particularly useful when the brush has a tall handle, a delicate natural-bristle face or a presentation box.
A simple sampling plan for buyers
You do not need to inspect every unit yourself, but you do need an agreed decision rule. A practical approach is:
- Approve a golden sample and written specification before mass production.
- Review a pre-production sample when the product includes a new material, mould, logo process or packaging format.
- Inspect a representative production sample before the order is released for shipment.
- Categorise defects as critical, major or minor in advance.
- Ask for inspection photos, counts and corrective action for any recurring defect.
For a first private-label brush order, allow enough time for this approval loop. A lower MOQ does not remove the need for sampling; it usually makes each design decision more important. For guidance on tooling, price breaks and sample planning, see custom hair brush manufacturing costs.
Questions to ask a brush factory before approving production
- Which component is most likely to vary in this design: bristles, cushion, handle finish or logo?
- How will bristle/pin retention be tested, and what result is considered acceptable?
- Can you provide several pre-production samples from the same process rather than one hand-finished sample?
- Which defects are checked at assembly, and which are checked only before packing?
- How will the brush be protected against bristle deformation and handle scratching in transit?
- Can the production lot and final-inspection record be matched to the shipment?
The best time to ask these questions is before the order enters production. Once the final carton is sealed, the choice is usually between accepting a compromise or delaying a launch.
From sample approval to a repeatable product
Good quality control is not a separate final step. It starts with a clear product brief, continues through material and sample approval, and ends with packaging and lot records that make the result repeatable.
If you are developing a private-label paddle, cushion or bristle brush, start with the custom paddle brush manufacturer page and send the product brief, target market, expected quantity, logo requirements and packaging reference. For a new design, a structured sample and prototype process is the safest way to turn this checklist into an approved production standard.